Intozi Vision AI | Compliant & Safer FMCG Manufacturing
Intozi Vision AI Platform delivers real-time AI video analytics for FMCG manufacturing, strengthening hygiene compliance, protecting product quality, and securing operations across every processing, packaging, and storage line.
Trusted by FMCG Manufacturing Leaders
We deliver AI-powered FMCG manufacturing solutions that are trusted by leading FMCG manufacturers to bring real-time hygiene, safety, and security intelligence to production plants and critical operations.


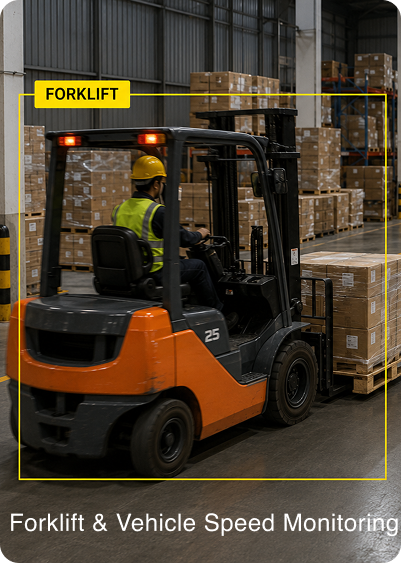
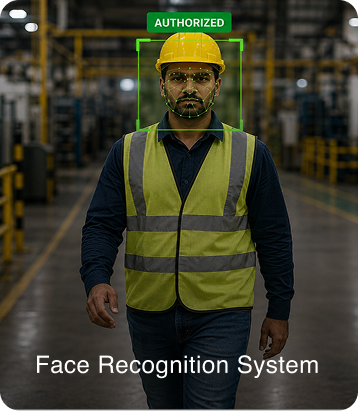
FMCG Manufacturing Video Analytics Use Cases
Meet Ikshana: The Intelligence Layer for FMCG Manufacturing
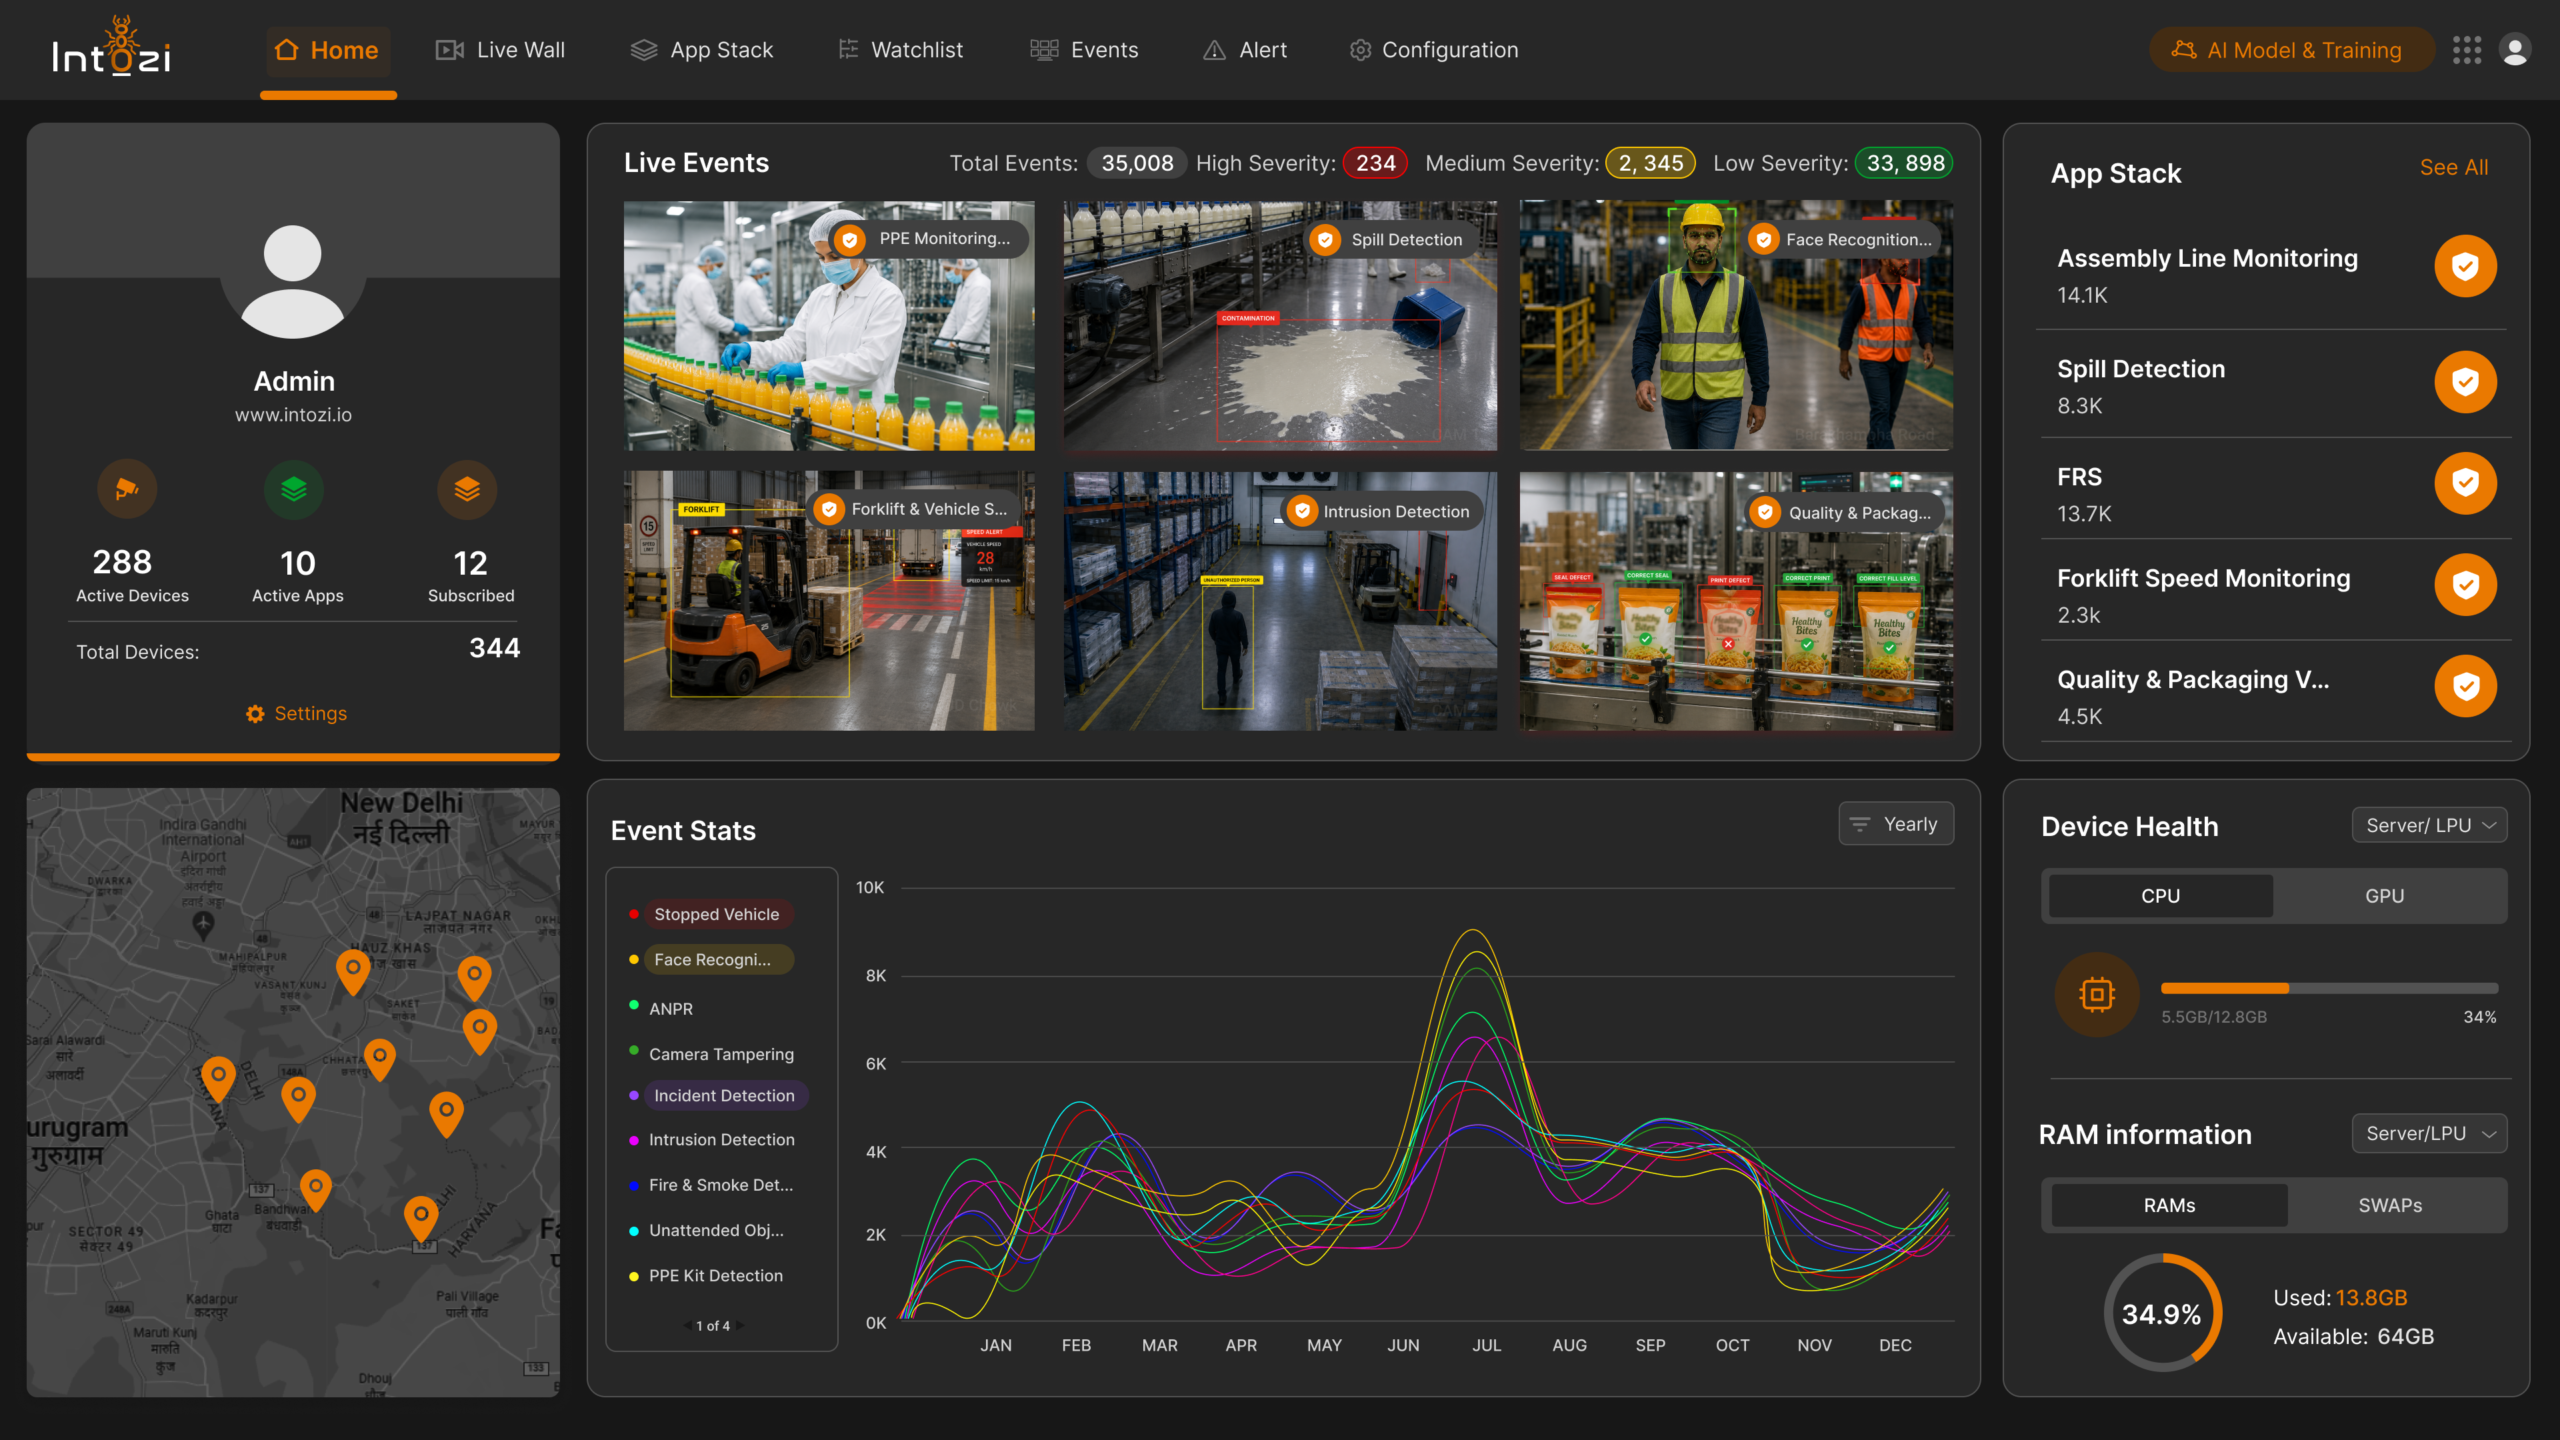
Ikshana, Intozi's AI video analytics solutions for FMCG manufacturing, brings real-time AI in FMCG manufacturing operations. Acting as a complete FMCG plant monitoring software, it converts existing IP/CCTV infrastructure into measurable hygiene, safety, and productivity metrics, giving plant heads and quality teams the visibility to make data-backed decisions and stay audit-ready across every shift, line, and storage zone.
Key capabilities
Enforce Hygiene & PPE Compliance
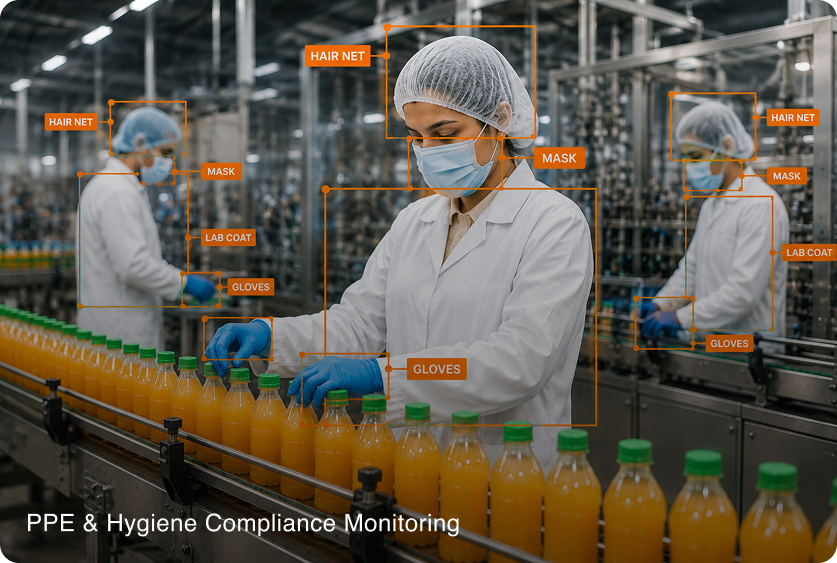
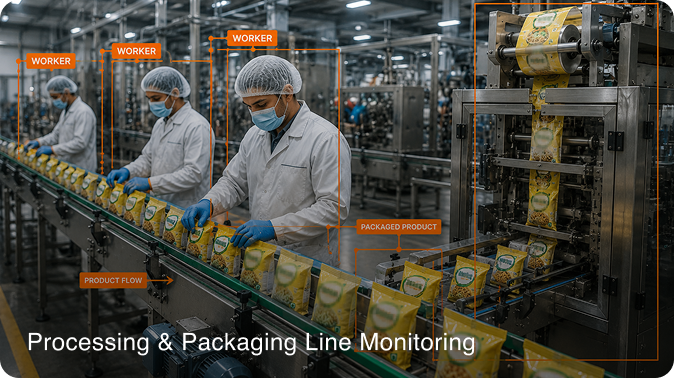
Automatically detects hairnet, mask, glove, and PPE violations on the processing floor, flagging non-compliant hygiene practices before they become a product safety risk.
Secure Warehouse & Cold Storage
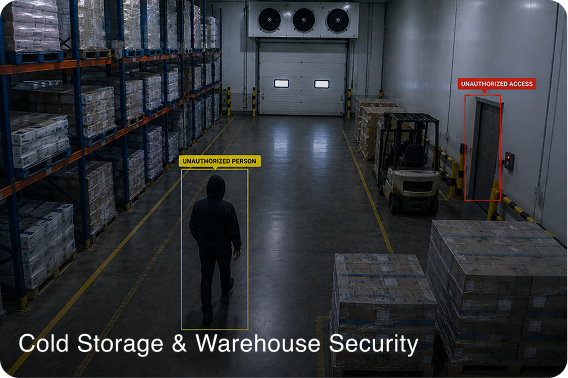
Monitor cold storage, loading docks, and warehouse zones for unauthorized access, temperature-sensitive handling risks, and after-hours activity.
Track Production & Packaging Visibility
Monitor processing lines, conveyors, and packaging stations from a single command center, with instant alerts to minimize downtime and improve throughput.
Accelerate Incident & Audit Response
Instantly retrieve relevant video evidence and AI-generated event timelines to reduce incident and compliance investigation time.
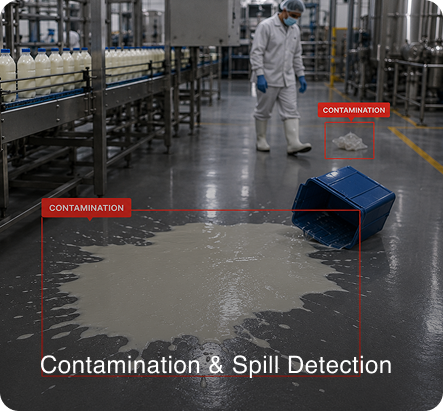
Spot Contamination & Hazards Instantly
Identify spills, unsafe behavior, and restricted-zone entry near processing and packaging areas with AI-based alerts, before they escalate into safety or quality incidents.
Maintain Plant-Wide Compliance Records
Digitally track procedure adherence across shifts and lines, maintaining audit-ready records to support HACCP, FSSAI, ISO 22000, and BRCGS reviews.
Why FMCG Manufacturing Leaders Choose Intozi
Vision AI for Safer, Compliant Plants
End-to-end operations monitoring with AI video analytics that detects PPE and hygiene non-adherence, contamination risks, and restricted-zone breaches before incidents occur.
Operational Excellence Across the Line
AI-based real-time analysis identifies bottlenecks across processing, packaging, and material flow, directly improving throughput and reducing downtime.
Zero-Disruption Deployment
Intozi plugs into your existing CCTV and control-room infrastructure, providing zero-code scalability and real-time intelligence without modifying infrastructure.
Make Your FMCG Plant More Compliant, Safer & More Productive
Intozi's FMCG video analytics continuously monitors processing lines, packaging stations, cold storage, and restricted zones to identify hygiene and safety risks, giving plant leaders the visibility to stay audit-ready while improving efficiency.
Frequently Asked Questions (FAQs)
Intozi’s FMCG video analytics continuously monitors processing lines, packaging stations, and warehouse and cold storage zones to identify hygiene, safety, and contamination risks, delivering complete AI solutions for FMCG manufacturing. This gives plant leaders the visibility needed to protect product quality while improving operational efficiency.
Yes. Ikshana, Intozi’s industrial AI monitoring system, integrates seamlessly with your existing CCTV and VMS infrastructure without hardware replacement, a fast, cost-effective upgrade for plants of any size or complexity.
By automatically detecting PPE and hygiene violations and restricted-zone breaches, Intozi’s AI hygiene compliance system for FMCG provides evidence-backed reports and digital compliance records to support audit readiness against HACCP, FSSAI, ISO 22000, and BRCGS frameworks.
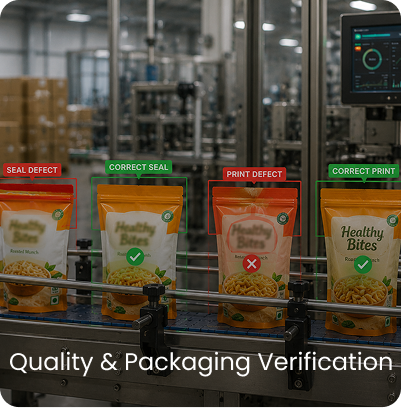
Absolutely. Intozi’s AI quality inspection for FMCG manufacturing enables processing and packaging line monitoring, product and packaging verification, cold storage and warehouse security, and vehicle entry/ANPR monitoring for continuous operational improvement.
Our infrastructure is STQC, CERT-IN, and ARAI compliant, delivering reliable AI safety monitoring for FMCG manufacturing and maintaining the highest standards of security and accuracy for FMCG manufacturing applications.